Chemicals & Materials
Continuous reactions and heat,
under precise control
Data scattered across power, LNG, steam and water is connected through an ontology, and an AI agent catches process shifts first and explains the cause. From unified multi-source energy monitoring to boiler air-ratio control and consolidated greenhouse gas management.
These are the problems on
chemical and materials sites today
- Several energy sources run at once
- Electricity, LNG, steam and water all feed the process
- Each source is aggregated separately
- The whole picture never forms
- Small changes upset quality
- Reactors, boilers and blowers run continuously
- A slight change carries straight through
- Process variables need precise control
- Air-fuel ratio, temperature, pressure and flow at once
- Going by feel cannot hold the optimum
- Energy cost and carbon rules tighten together
- Simple monitoring is no longer enough
This is how
Refinery solves it
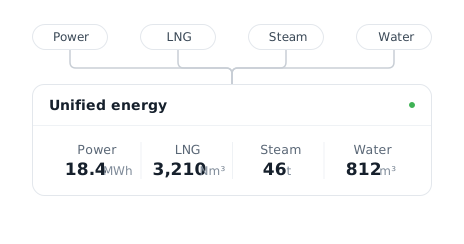
Unified electricity, LNG, steam and water monitoring
- Problem
- Multiple energy sources, each aggregated separately
- Approach
- Electricity, LNG, steam, water and consumption by asset are connected through an ontology into one structure, so the whole energy flow sits on one screen.
- Outcome
- Usage patterns made visible by energy source
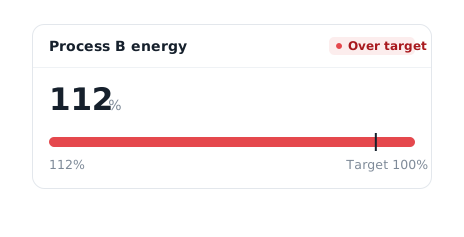
Energy targets and overrun alerts
- Problem
- Over-consumption confirmed only after the fact
- Approach
- Targets are set by asset and process, and overrun is raised in real time.
- Outcome
- Over-consumption prevented and immediate response in place
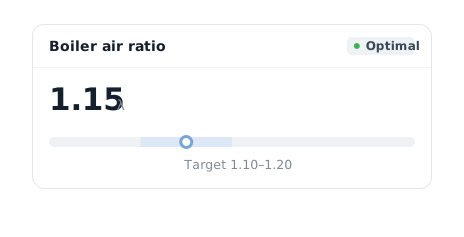
Air-fuel-ratio-based blower VFD control for thermal fluid boilers
- Problem
- Thermal fluid boiler air-fuel ratio set by feel
- Approach
- The blower VFD is controlled against the thermal fluid boiler air-fuel ratio so the optimum is held.
- Outcome
- Better combustion efficiency and lower energy cost
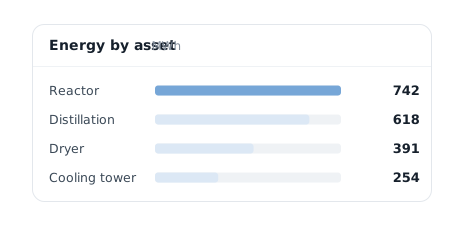
Energy use analysis by asset
- Problem
- No way to tell which assets are eating up the energy
- Approach
- Energy is metered separately by asset and compared on equal terms.
- Outcome
- Energy-intensive assets identified
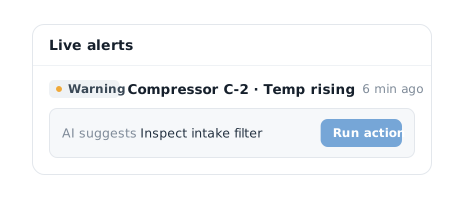
Air compressor state and operating parameter monitoring
- Problem
- Compressor anomalies that surface only after a stop
- Approach
- An AI agent reads compressor state and operating parameters together to catch early signs in patterns that differ from the norm, and proposes both the cause and the next action.
- Outcome
- Steadier equipment operation and more efficient maintenance
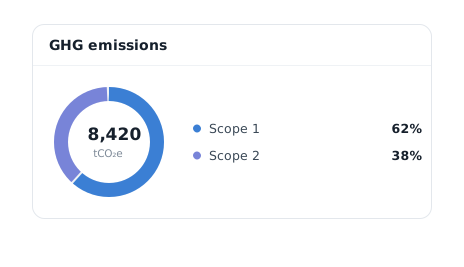
Unified greenhouse gas emissions management
- Problem
- Manual aggregation of emissions and regulatory reports
- Approach
- Emission metrics are aggregated automatically from field data into reports traceable to their source.
- Outcome
- Carbon compliance and energy performance management
How it fits together
How field data gains meaning and turns into a decision.
- Reactors
- thermal fluid boilers
- blowers
- compressor sensors
- SCADA
- PLC
- Plant EMS
- Modbus
- Serial
- 4–20 mA
- Ontology
- AI agent
- rules and automation
- Energy dashboard
- target alerts
- emission reports
Where SCADA or a plant EMS already exists, a layer sits on top of it and integrates bidirectionally rather than replacing it. Where none exists, collection is built from the ground up.
Systems we connect to
The systems and protocols commonly used on chemical sites.
Systems not listed here can still be connected over standard protocols and APIs. Get in touch and we will walk through it.
What you gain
Benefits across operations, engineering and management.
Target-based energy management
Targets are set and overrun is raised in real time.
Optimal air-fuel ratio control
Combustion data holds the ratio at its optimum.
Energy variance by asset
Energy is split asset by asset to pin the heavy consumers.
Early detection of energy anomalies
Patterns that differ from the norm are noticed first.
Carbon compliance
Emissions are aggregated automatically, with sources traceable.