Machinery & Plant
Large equipment and process,
controlled together in real time
Data scattered across large equipment running around the clock and several energy sources is connected through an ontology, and an AI agent catches anomalies first and explains the cause. From demand-matched air compressor control to HVAC inverter control and consolidated carbon monitoring.
These are the problems on
machinery and plant sites today
- Several energy sources run at once
- Compressed air, electricity, heating, cooling and HVAC all run
- Where the energy goes never becomes clear
- Equipment is tightly coupled
- One machine carries through to the whole process
- The plant cannot pause
- Process conditions must still hold
- No obvious moment to intervene
- Aging, cost and rules arrive at once
- Equipment keeps aging
- Energy cost keeps rising
- Equipment and energy must be seen as one
This is how
Refinery solves it
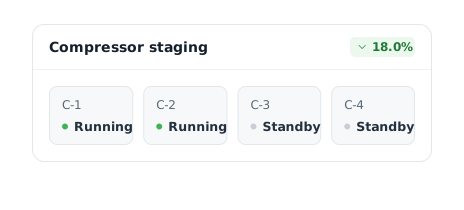
Demand-based compressed air control and monitoring
- Problem
- Shared utilities that keep running when demand drops
- Approach
- Real demand is read and discharge pressure and unit staging are matched to what is needed.
- Outcome
- Lower energy use and longer equipment life
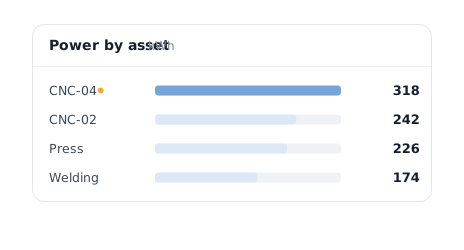
Live power analysis by asset
- Problem
- Energy use grouped in clusters and impossible to separate
- Approach
- An AI agent watches consumption by asset in real time to catch use that departs from the usual pattern, and proposes both the cause and the next action.
- Outcome
- Energy-intensive assets identified and operations improved
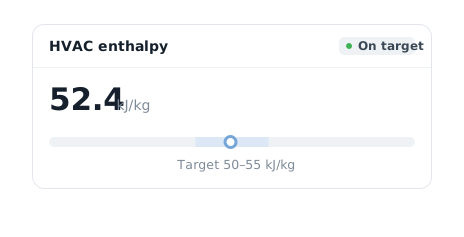
Enthalpy-based HVAC VFD control
- Problem
- HVAC running fixed, regardless of outdoor conditions
- Approach
- Line temperature and humidity are converted to enthalpy, and the HVAC VFD is controlled to hold the target.
- Outcome
- Steadier process environment and lower heating and cooling energy
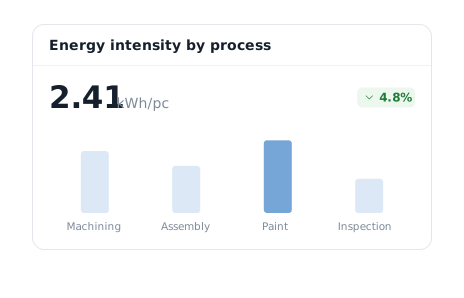
Energy intensity tied to output
- Problem
- No baseline for comparing efficiency against production
- Approach
- Production records and energy by asset are connected through an ontology into one structure, and intensity by process is derived automatically.
- Outcome
- Process efficiency made visible and cost structure improved
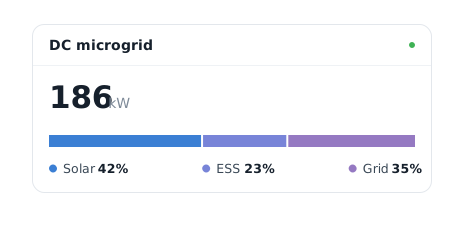
DC-microgrid-based equipment control
- Problem
- Equipment operation left unsteady, tied to a single grid feed
- Approach
- On-site generation and the grid are read together to distribute power across equipment.
- Outcome
- Lower fuel cost and steadier energy operations
Unified carbon emission monitoring
- Problem
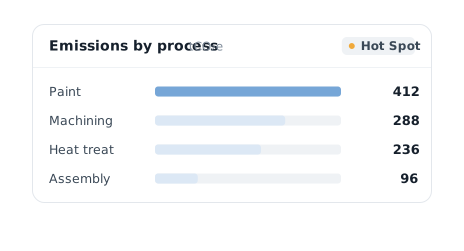
- Emissions never broken out by process
- Approach
- Emissions are derived per process from energy data and hot spots are marked.
- Outcome
- Carbon compliance and energy performance management
How it fits together
How field data gains meaning and turns into a decision.
- Air compressors
- HVAC
- cooling equipment
- large machinery sensors
- Plant EMS
- SCADA
- PLC
- ERP
- Modbus
- BACnet
- Ontology
- AI agent
- rules and automation
- Utility dashboard
- energy intensity reports
- emission management
Where a plant EMS or SCADA already exists, a layer sits on top of it and integrates bidirectionally rather than replacing it. Where none exists, collection is built from the ground up.
Systems we connect to
The systems and protocols commonly used on machinery and plant sites.
Systems not listed here can still be connected over standard protocols and APIs. Get in touch and we will walk through it.
What you gain
Benefits across operations, engineering and management.
Demand-based compressed air control
Shared utilities run only as much as actual demand requires.
Savings from HVAC VFD control
Load follows enthalpy, cutting heating and cooling energy.
Condition-based maintenance
Condition data sets the moment to intervene.
Efficiency analysis tied to output
Output and energy are joined to compare efficiency by process.
Lower fuel cost
A DC microgrid distributes power and steadies operations at the same time.
Carbon compliance
Emissions are derived per process so hot spots come first.