Electronics & Precision
Uninterrupted power and microenvironment,
protected by one system
Data scattered across production equipment, power and the microenvironment is connected through an ontology, and an AI agent catches outages and environmental drift first and explains the cause. From peak demand monitoring to UPS-linked outage alarms and real-time temperature and humidity control.
These are the problems on
electronics and precision sites today
- Equipment reacts to the smallest change
- Sensitive to temperature shifts
- Power quality leaves its mark on the process
- A power outage becomes a defect
- A momentary outage stops the line
- Equipment anomalies turn into defective product
- Operating factors are tangled together
- Peak demand and UPS response sit side by side
- Temperature, humidity and alarms run apart
- Safety and fire systems are expected in the same structure
- High-mix, low-volume production splits the lines
- Process-level energy management gets harder
This is how
Refinery solves it
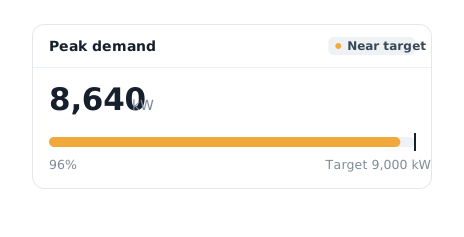
Live peak demand monitoring and load control
- Problem
- Peak demand confirmed only once the peak has passed
- Approach
- Linked to a demand controller, the system holds load inside the target and raises an alert before the peak is exceeded.
- Outcome
- Lower electricity charges and reduced peak risk
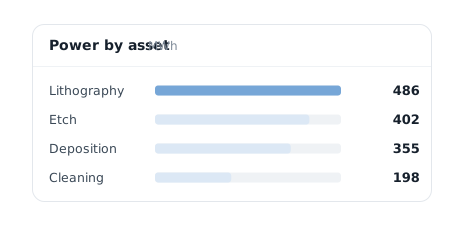
Power usage patterns by asset
- Problem
- No way to tell which equipment draws the most power
- Approach
- Assets and processes are connected through an ontology, so each signal is given meaning — which asset it belongs to and what it measures — and power can be compared on equal terms.
- Outcome
- Energy-intensive processes identified
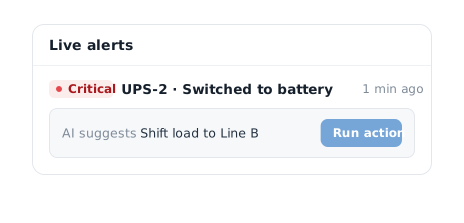
UPS-linked outage detection and alerts
- Problem
- Outage and UPS transfer events logged apart from equipment history
- Approach
- An AI agent reads power quality and UPS events on the same timeline as equipment state, and proposes both the scope of impact and the next action.
- Outcome
- Uninterrupted operation and minimal line stops
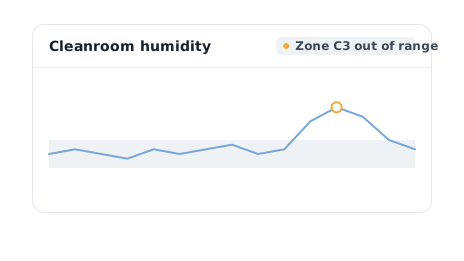
Live temperature, humidity and process heater monitoring
- Problem
- Invisible temperature and humidity drift between lines
- Approach
- Process environment data is collected zone by zone and each point outside the band is flagged immediately.
- Outcome
- Steadier process quality
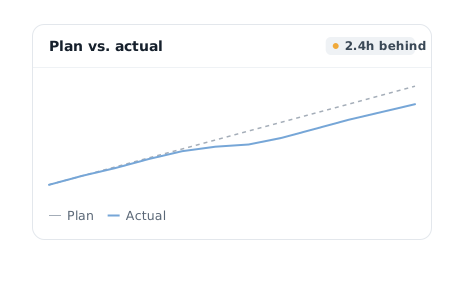
Equipment state against the production plan
- Problem
- Plan and actual equipment operation drifting apart unnoticed
- Approach
- Production plans are linked to equipment operation and alarm history to trace response lag.
- Outcome
- More accurate production forecasting
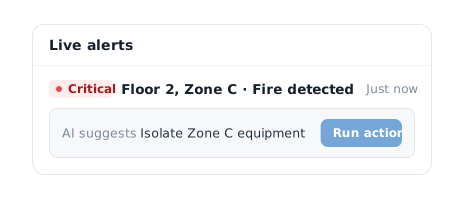
EHS and fire monitoring in the same alert stream
- Problem
- Safety systems running apart from equipment monitoring
- Approach
- EHS and fire detection signals are folded into the same alert structure as equipment alarms.
- Outcome
- Safety incidents prevented
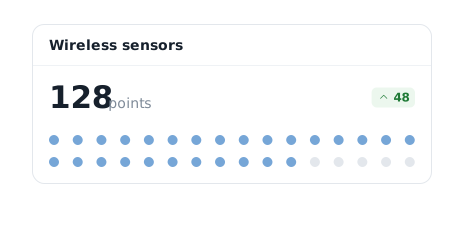
Wireless sensor deployment for power and environment
- Problem
- Measurement points that are hard to add because they need cabling
- Approach
- Wireless sensors extend power and environment coverage without new cable runs.
- Outcome
- Lower build cost and room to scale
How it fits together
How field data gains meaning and turns into a decision.
- Switchgear
- UPS
- temperature and humidity
- process tool sensors
- MES
- SCADA
- UPS
- demand controllers
- Modbus
- OPC UA
- Ontology
- AI agent
- rules and automation
- Power quality dashboard
- outage alerts
- environment monitoring
Where MES or SCADA already exists, a layer sits on top of itand integrates bidirectionally rather than replacing it.Where none exists, collection is built from the ground up.
Systems we connect to
The systems and protocolscommonly used on electronics sites.
Systems not listed here can still be connectedover standard protocols and APIs.Get in touch and we will walk through it.
What you gain
Benefits across operations, engineering and management.
Load trimmed before the peak
Load is lowered ahead of the peak rather than after it.
Immediate alerts on equipment anomalies
When an anomaly appears, the responsible engineer is alerted at once.
Live process environment monitoring
Temperature and humidity are tracked zone by zone in real time.
Operation tracked against the plan
Production plan and equipment response are placed side by side.
Safety incidents prevented
EHS and fire signals join equipment alarms in one alert structure.
Room to scale
Wireless sensors extend coverage without new cable runs.